
High-Precision Profile & Pipe Extrusion Line Units
Explore our heavy-duty extruders, calibration water tanks, haul-off pullers, and specialized forming systems engineered to run 24/7 with minimal scrap.

Custom Corrugated Forming Machine Product, Products
Explore Line Details
Custom Precision Medical Tube Extrusion Line Manufacturers, Factory
Explore Line Details
China Vacuum Calibration Cooling Table Manufacturer, Products
Explore Line Details
China QYP Series Belt Puller Manufacturer, Factory
Explore Line Details
China UHMWPE Profile Extrusion Line Manufacturer, Manufacturers
Explore Line Details
China PA (Nylon) Precision Tube Extrusion Line Factories, Product
Explore Line Details
Custom Vacuum Calibration Spraying Cooling Tank Factory, Products
Explore Line Details
China ABS,PP,PVC Automobile Profile Extrusion Line Manufacturer, Products
Explore Line DetailsThe Evolution of Precision Plastic Profile Extrusion: Micro-Tolerances & Advanced Melt Rheology
Over the last decade, plastic profile extrusion has transitioned from traditional commodity processing into a highly calibrated science governed by thermodynamics, non-Newtonian polymer melt rheology, and real-time closed-loop control. Today's global OEMs require thermoplastic and fluoro-elastomeric profiles to withstand high mechanical loads, aggressive chemical exposures, and stringent thermal variations.
At BAOD EXTRUSION (Jiangsu Baodie Automation Equipment Co., Ltd.), our legacy stems from the KINGSWEL GROUP, which honed 18 years of specialized machine fabrication in Taiwan prior to establishing operations in mainland China in 1999. Since the founding of the BAOD EXTRUSION brand in 2002, our engineering center has focused on solving dimensional drift, wall thickness variance, and surface shear stress in complex multi-lumen hollow sections, co-extrusion seals, and structural engineering profiles.
Advanced Rheological Die Tooling
CAD/CAM flow simulation eliminates dead zones, maintains balanced volumetric distribution, and prevents polymer degradation across complex cross-sections.
- Streamlined coat-hanger and spiral die topologies
- Custom nitrided & mirror-polished tool steel (38CrMoAlA)
- Individual thermal zone tuning within ±0.5°C
High-Efficiency Plastification
Custom barrier screw geometries maximize shear homogenization while mitigating melt thermal peaks, elevating line speed without compromising polymer chain integrity.
- Dedicated L/D ratios (25:1 to 34:1) tailored to polymer type
- Bimetallic barrels for abrasive fluoropolymer processing
- Optimized grooved feed bush for linear output pressure
Intelligent Industry 4.0 PLC
Fully integrated Siemens or Beckhoff control architectures synchronize extruders, cooling troughs, caterpillar pullers, and flying servo rotary cutters.
- OPC-UA and industrial Ethernet compatibility
- Real-time scrap alerting and auto-speed trimming
- Comprehensive recipe storage with one-touch recall
Robust Sizing & Cooling Mechanics
Multi-chamber vacuum sizing and high-turbulence spray calibration ensure freeze-in geometry stability and eradicate residual stresses inside hollow profiles.
- Closed-loop PID vacuum level control (±0.1 kPa)
- Dual-axis mechanical alignment for zero pull distortion
- Anti-corrosion SS304/SS316 tank design
Enterprise Sourcing Demands: What Tier-1 OEMs Require
Procuring profile extrusion lines requires technical qualification across several operational metrics. Overseas engineering directors and procurement leads scrutinize reliability and scrap margins.
Statistical Process Capability (Cpk > 1.67)
Automotive fluid line and medical catheter manufacturers do not tolerate nominal deviation. Extrusion downstream units must feature closed-loop ultrasonic wall measuring and multi-axis laser gauges that continuously feedback into the puller servo drive.
Multi-Material Adhesion & Co-Extrusion
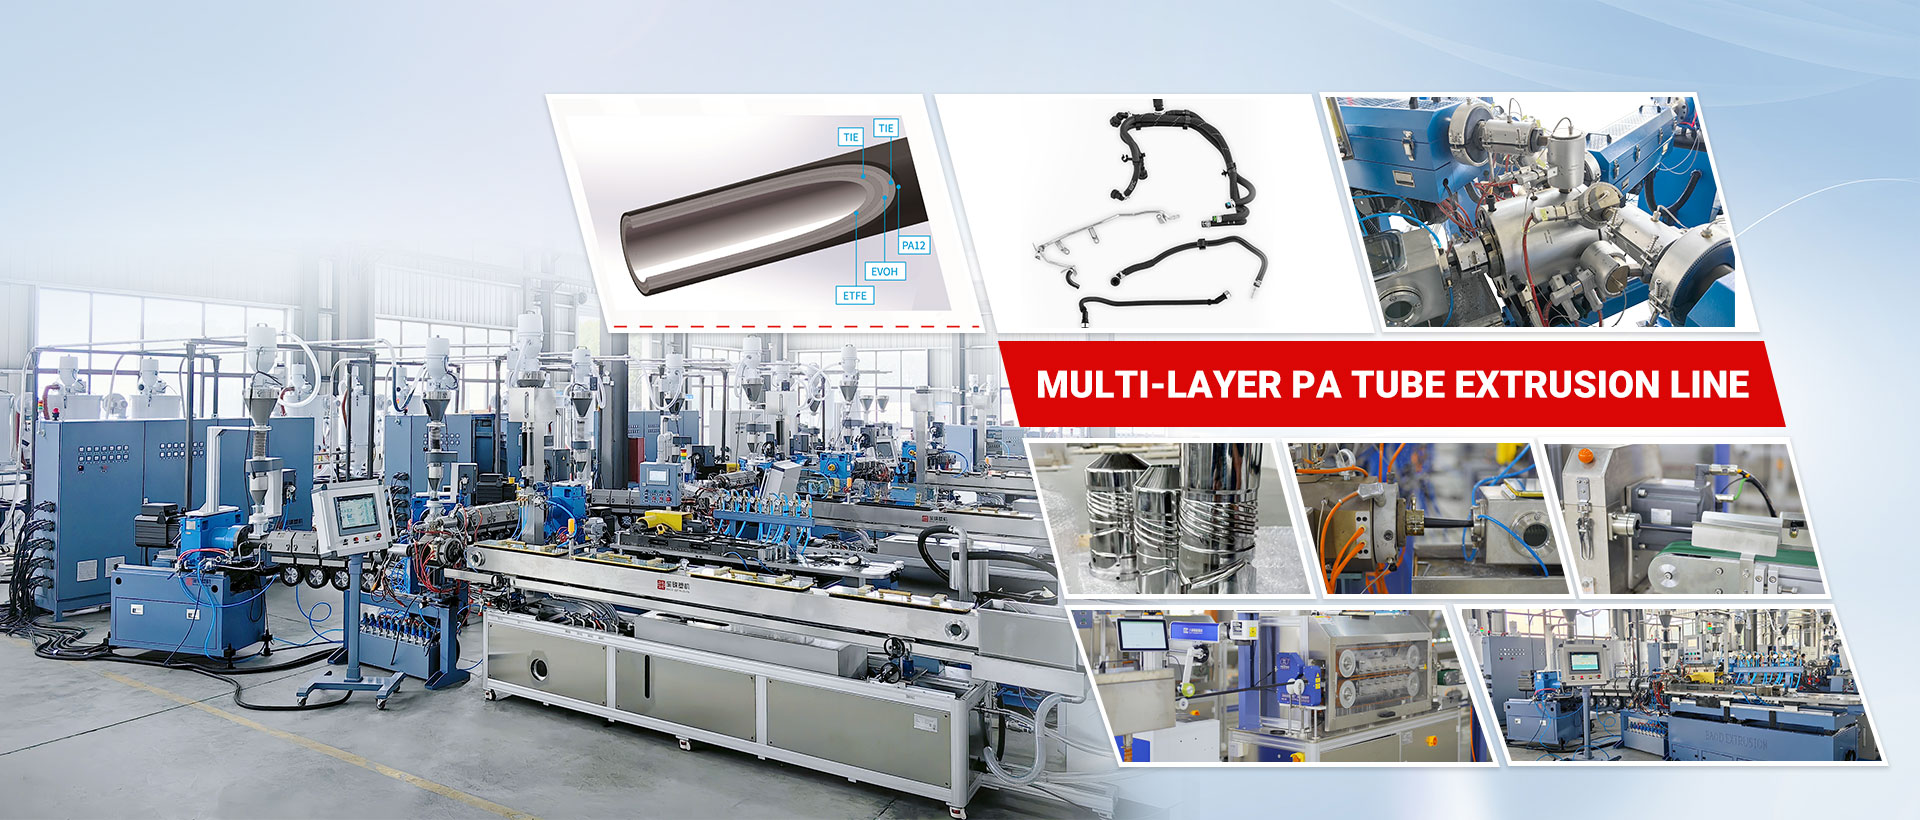
Global automakers demand co-extruded TPV/PP and PA/EVOH structures with exact layer boundaries. Tooling must deliver laminar fluid flow without interfacial instability, ensuring strict chemical bonding and zero risk of delamination.
Rapid Changeover & Reduced Tool Wear
Shorter batch runs demand quick-change calibration dies and modular sizing sleeves. Extrusion barrels equipped with bimetallic tungsten carbide linings withstand filler content including carbon black, glass fibers, and ceramic powders.
| Engineering Specification | Conventional Extrusion Lines | BAOD Industry 4.0 Precision Lines | Customer Operational Impact |
|---|---|---|---|
| Melt Temperature Uniformity | ±2.5°C to ±3.5°C | ±0.5°C across all barrel zones | Eliminates molecular degradation and wall thickness surges. |
| Puller Speed Synchronization | Analog voltage ±1.0% fluctuation | Digital CANopen/EtherCAT ±0.05% | Guarantees longitudinal dimension consistency during coiling. |
| Tool Steel Metallurgy | Standard 45# or 40Cr steel | 38CrMoAlA (Nitrided) / DIN 1.2316 | 300% longer mold lifespan with zero corrosion under halogen exposure. |
| Scrap Rate at Start-Up | 12% - 18% startup resin waste | < 3.5% automated ramping waste | Saves tens of thousands of USD annually in virgin engineering resins. |
China Factory 4.0: Jiangsu Baodie's Integrated Efficiency Advantage
Navigating global supply chain volatility requires equipment manufacturing partners that control core production processes in-house. Operating from our modern 16,000 m² manufacturing facility in Haian, Nantong, Jiangsu, BAOD integrates CNC die machining, electrical cabinet wiring, screw hardening, and line assembly within a single traceable facility.
By blending Taiwan-origin precision engineering heritage with the Yangtze River Delta's integrated industrial supply ecosystem, BAOD eliminates reliance on third-party subcontractors. We produce complete extrusion packages—from screw plastification units to vacuum calibration tables, pullers, and flying cutters—with short lead times and strict quality control.
High-Precision 5-Axis CNC Tooling
All extrusion heads, calibrating sleeves, and water tanks are cut using 5-axis machining centers. This guarantees mirror-like finishes (Ra < 0.05 μm) on flow channels, reducing polymer hang-up and color changeover duration.
Factory Acceptance Trials (FAT) With Virgin Resin
Prior to sea freight dispatch, every custom line undergoes comprehensive test runs utilizing customer-specified resin compounds. Real product runs verify dimensional stability, melt homogeneity, and downstream synchronization.
Global After-Sales & Remote Diagnostics
Equipped with secure cloud-gateway modules, BAOD engineers provide real-time software diagnostics, firmware optimization, and troubleshooting for overseas clients, backed by our dedicated Global Service program.
Worldwide Industrial Realities & Localized Use Cases
From electric vehicle battery thermal management to sterile surgical devices and industrial chemical transport, custom extruded plastics serve critical roles across modern infrastructure.
Automotive Thermal Management & Fluid Handling
EV platforms require tight-tolerance fluid transfer tubes, multilayer corrugated cooling hoses, and fuel vapor lines. Materials like PA11, PA12, and PVDF demand multi-layer co-extrusion dies that maintain consistent barrier properties.
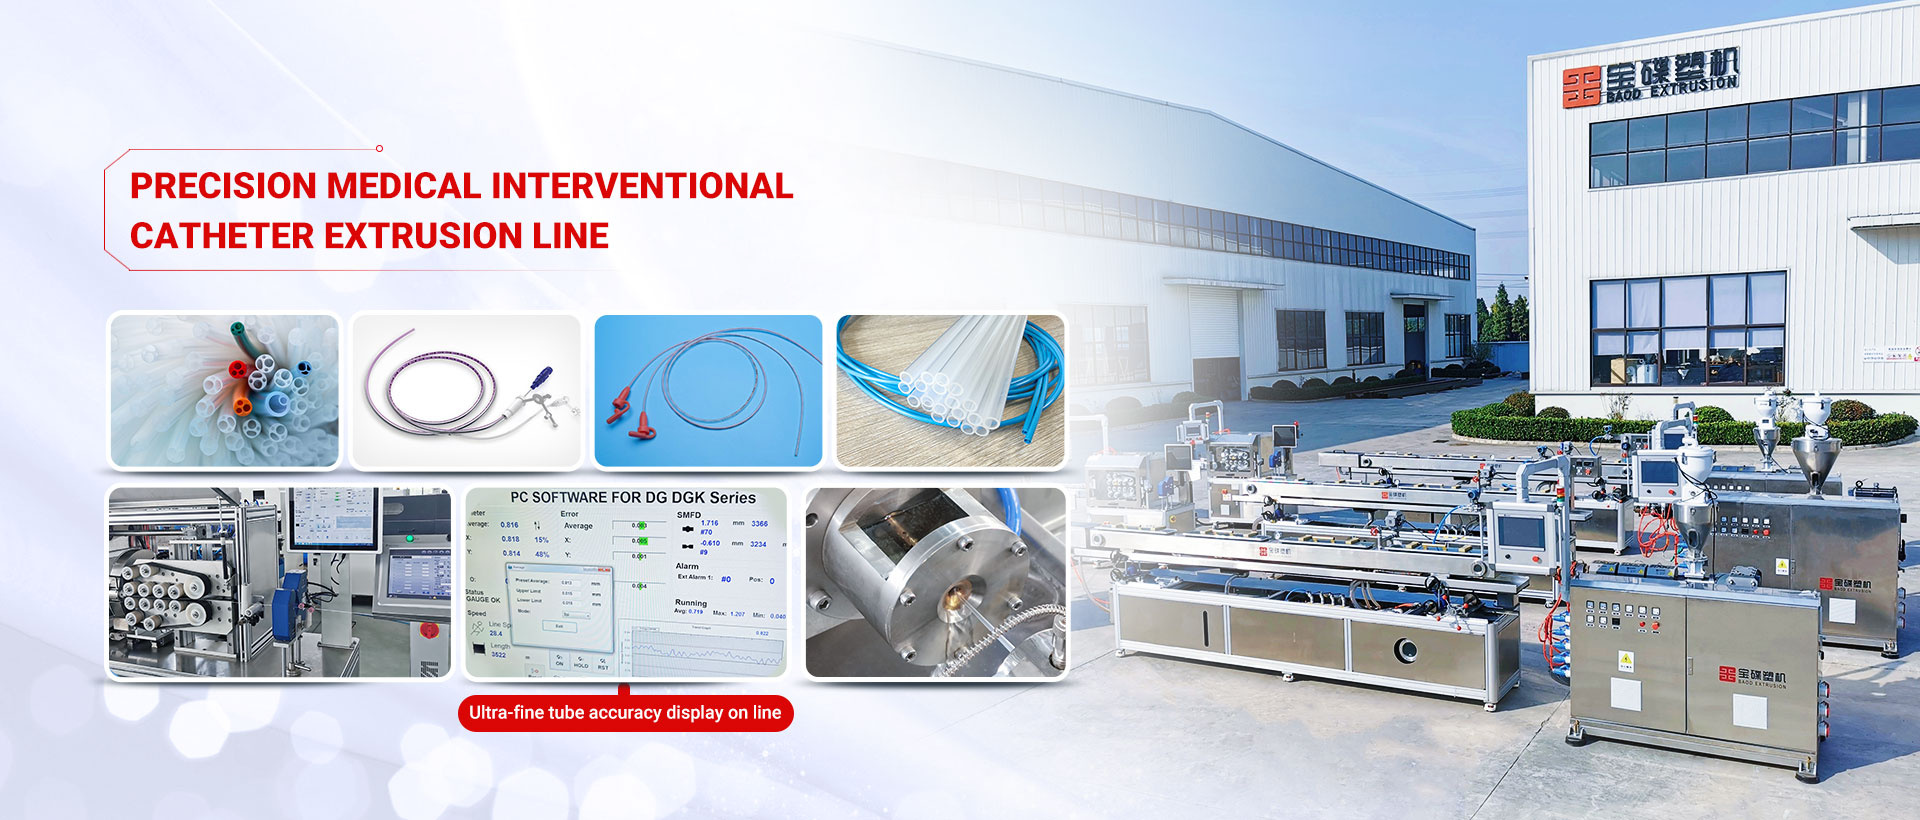
Medical Disposable Tubing & Multi-Lumen Catheters
Cleanroom extrusion lines running medical SPVC, TPU, and PEEK require sanitary stainless-steel cooling troughs, cleanroom air filters, and precision micro-extruders to shape catheters without ovality or lumen collapse.
Automotive Sealing Systems & Technical Profiles
TPV/PVC co-extrusion lines produce multi-durometer sealing profiles for doors, windows, and glass-run channels. These components block wind turbulence, environmental dust, and road noise (NVH) in passenger cars.
Mining Shock Tubes & Industrial Conduits
Lines engineered for non-electric detonating shock tubes deposit reactive inner-wall dusting agents at tight tolerances, providing safe propagation velocity across open-pit mining and infrastructure projects.
Global Market Dynamics: North America, Europe, and Emerging Manufacturing Hubs
The global market for plastic profile extrusion machinery is shaped by distinct regional drivers:
North America
High demand for automated optical fiber microducts (HDPE/Silicone), telecommunications conduit systems, and construction window profiles with high UV-stabilizer loading.
Europe & UK
Focus on circular economy mandates, post-consumer resin (PCR) compounding lines, bio-based polyamide tubes, and low-energy servo heating systems.
Asia-Pacific & Latin America
Rapid EV platform expansion, requiring cost-effective localized manufacturing of TPV sealing strips, smooth and corrugated fuel hoses, and medical infusion lines.
Automotive, Medical & Specialized Industrial Extrusion Solutions
Continuous co-extrusion, multi-layer corrugated composite hoses, UHMWPE handling lines, and custom cable/pipe coating systems.

China TPV Knitting Compostie Hose Extrusion Line Factory, Factories
Explore Line Details
Custom TKC Series Crawler-Type Puller Product, Products
Explore Line Details
Custom HDPE Silicone Core Tube (Micro Duct) Extrusion Line Factory, Products
Explore Line Details
China Multi-Layer PA Smooth / Corrugated Hose/ Tube Extrusion Line Manufacturers, Factories
Explore Line Details
Custom Shock Tube/Non-electric Detonator Extrusion Line Product, Products
Explore Line Details
Custom Metal Pipe Coating Extrusion Line Manufacturer, Manufacturers
Explore Line Details
China Precision Profile Extrusion Line Manufacturers, Products
Explore Line Details
China LDPE,HDPE,PP Precision Tube Extrusion Line Manufacturer, Factory
Explore Line DetailsFrom Drawing to Commercial Production: 5 Engineering Milestones
Every extrusion system engineered at our Jiangsu plant follows a structured five-stage validation lifecycle, ensuring turn-key readiness upon arrival at your overseas facility:
Material Rheology & CAD Die Channel Simulation
Melt flow indexing (MFI), thermal shrinkage calculations, and CFD flow profiling define die and mandrel channel geometries.
Precision Machining & Nitriding Treatment
38CrMoAlA barrels receive precision wire cutting, deep-hole boring, polishing, and 72-hour gas nitriding (HV ≥ 950).
Assembly & Synchronized PLC Architecture Integration
Extruders, vacuum calibration cooling tables, haul-offs, and rotary cutters are aligned on a continuous ground datum.
FAT Material Trials & Continuous Running Audits
Extrusion lines run at design speeds using customer-specified resins. Profiles undergo continuous laser micrometer Cpk qualification.
Global Commissioning & On-Site Training
Field service engineers oversee on-site positioning, utility tie-ins, line balancing, and operator training programs.
Technical Proposal Request Checklist
Providing these technical details upfront ensures an accurate tooling proposal within 24 business hours:
- Cross-Sectional Drawing (CAD/PDF): Detailed dimensions, wall thicknesses, and tolerance bands (±mm).
- Resin Formulation & Grade: Polymer datasheet, filler ratios (talc/glass fiber), and MFI values.
- Production Throughput: Target line speed (m/min) or target mass throughput (kg/hour).
- Downstream Requirements: Planetary cutting, swarfless chipless shear, auto coiling, or inkjet printing.
- Utility Infrastructure: Facility voltage, frequency (e.g. 480V 60Hz), and available footprint dimensions.
Frequently Asked Questions on Custom Profile Extrusion
In-depth responses covering rheological engineering, vacuum sizing, co-extrusion parameters, and international line validation.
What polymer families and specialty resins can BAOD extrusion lines process?
How does BAOD maintain cross-sectional tolerances within ±0.02 mm on hollow profiles?
What are the key technical challenges in co-extruding multi-durometer TPV and PVC profiles?
How do your Chinese extrusion lines compare against top German or Italian equipment?
Can BAOD provide custom downstream cutting and coiling units for existing lines?
What documentation and compliance certifications accompany international shipments?
Ready to Engineer Your Custom Extrusion Line?
Collaborate directly with our senior application engineers. We evaluate your cross-section drawings, resin datasheets, and production volumes to deliver an optimized manufacturing solution.